Product Introduction
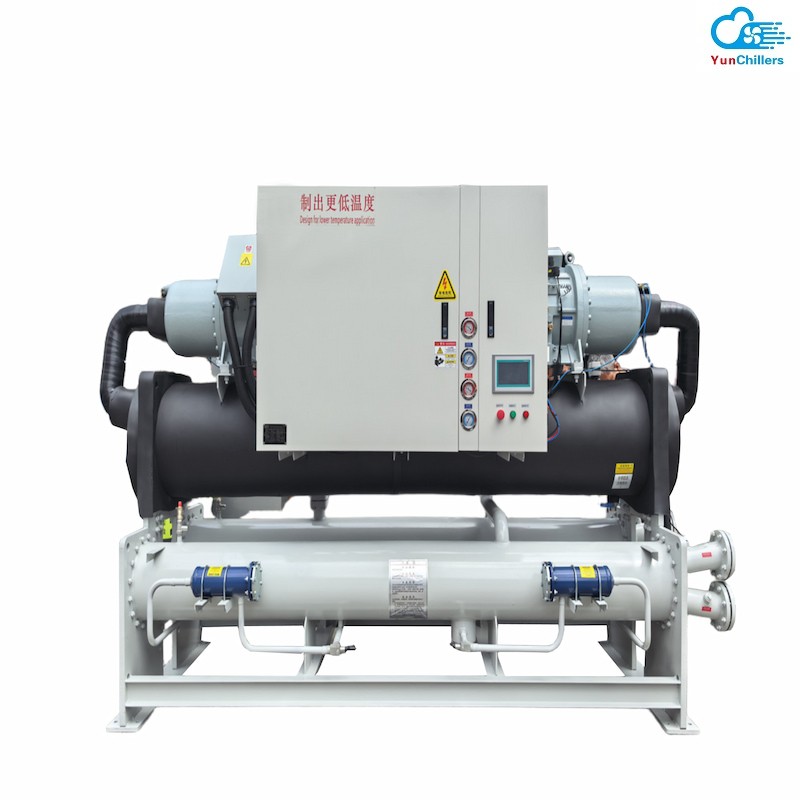
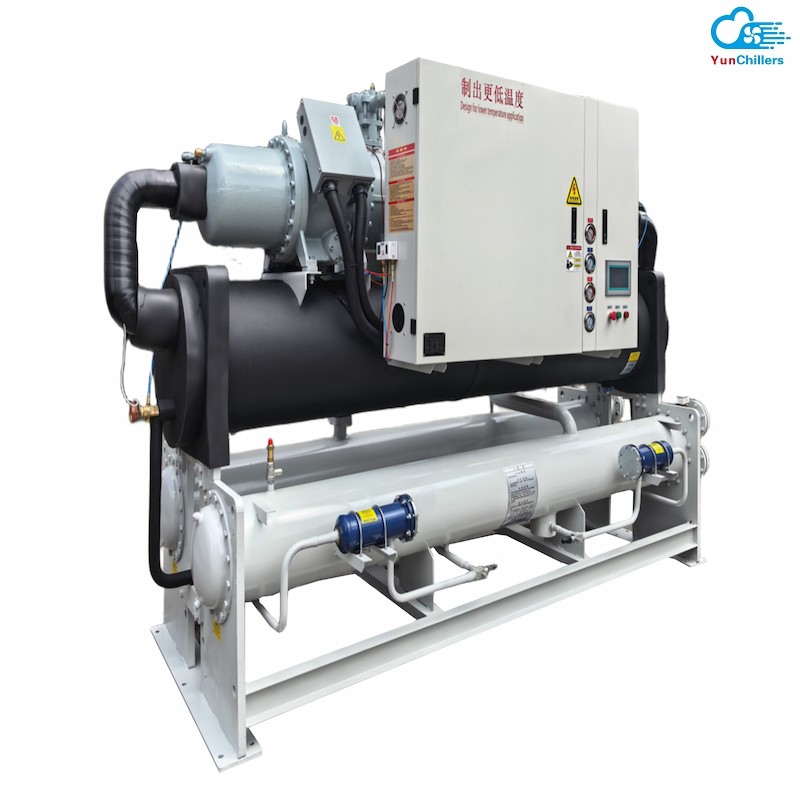
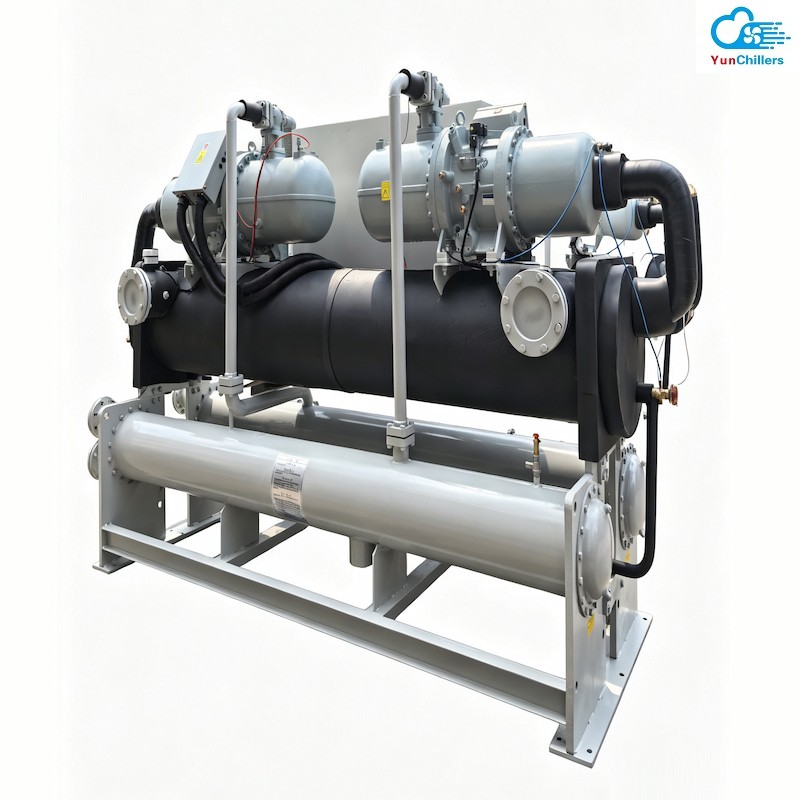
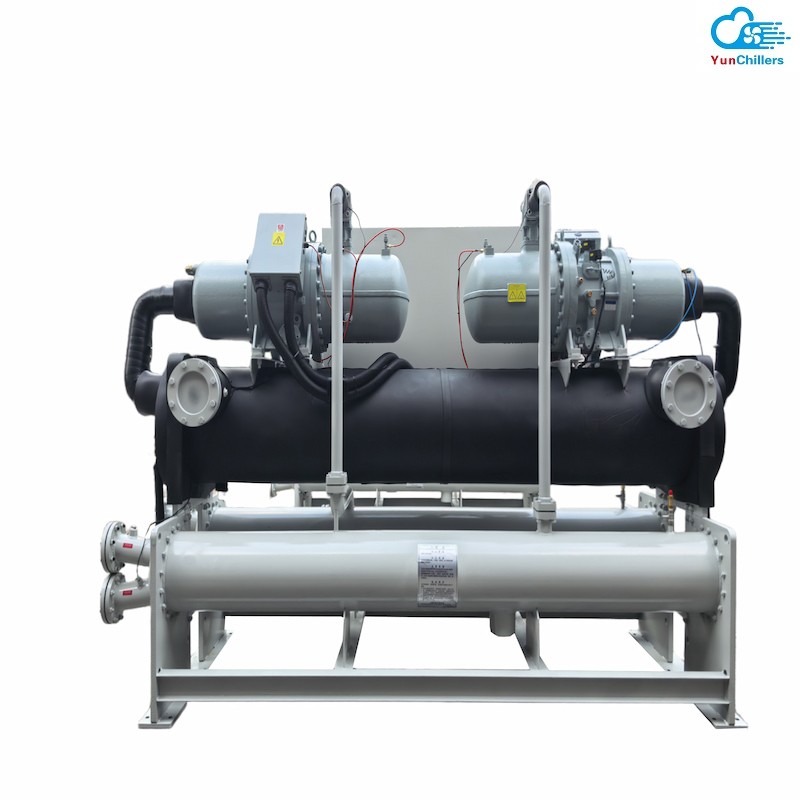
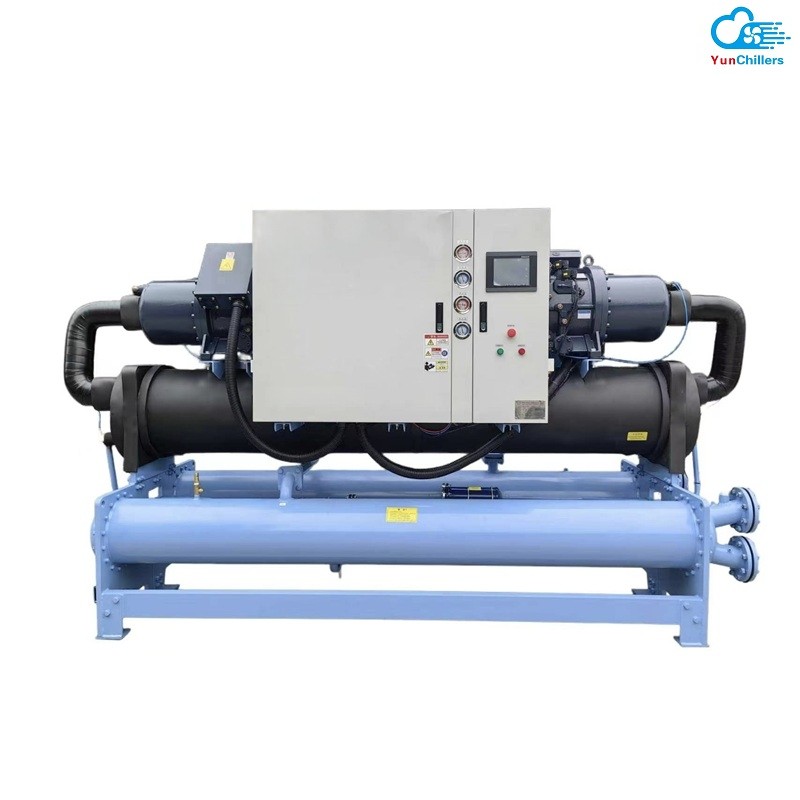
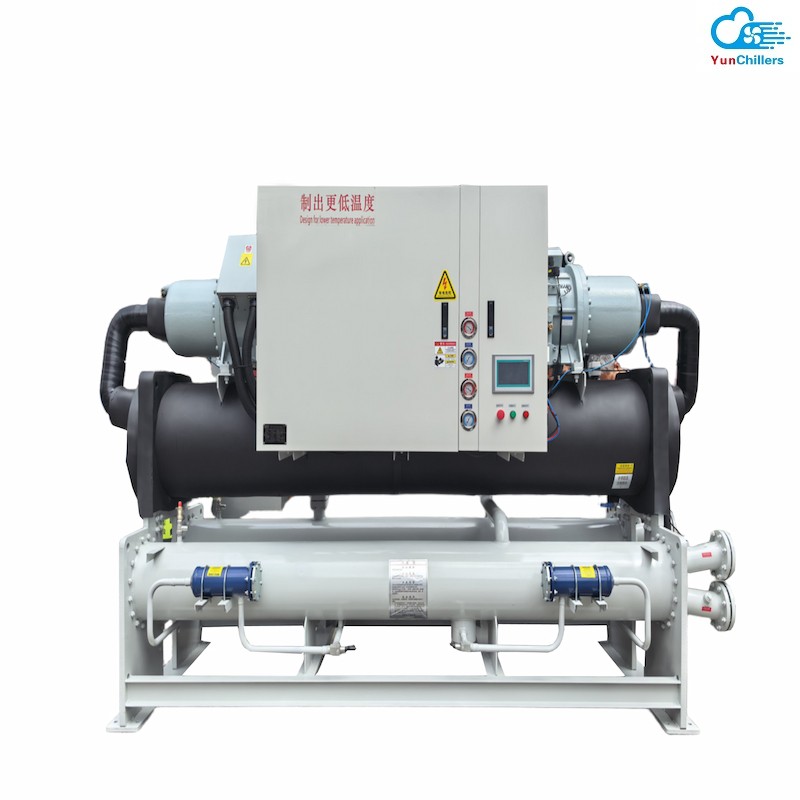
Engineered for pharmaceutical facilities and cleanrooms, this total heat recovery chiller unit combines precise process cooling with heat recovery. While supplying chilled water to reactors and cleanroom circuits, the system reclaims condenser heat for air pretreatment or reheat loops, working alongside total heat recovery AHU installations. It offers a cGMP-compliant pharmaceutical industrial chiller designed to reduce overall operating costs.
Product Advantages
Heat Recovery Efficiency: Operating as a total heat recovery chiller unit, the system reclaims condenser waste heat to supply warm water loops. This setup, paired with a heat recovery industrial chiller configuration, reduces cooling tower duty and auxiliary heating demand to lower facility operating expenses.
Stable Process Temperature Control: Built for temperature-sensitive production, the unit operates alongside a pharmaceutical water-cooled chiller plant to deliver stable fluid supply temperatures, supporting batch consistency across fermentation and synthesis processes.
Cross-Contamination Protection: Built with isolated fluid circuits, this bio-pharmaceutical heat recovery unit prevents cross-contamination between cooling and heating loops, complying with stringent cleanroom hygienic standards.
Continuous Operational Reliability: Designed for continuous duty, the onboard controls synchronize with industrial chiller units and downstream cleanroom total heat recovery unit controls to adjust output based on real-time loads while minimizing maintenance downtime.
 Get a Quote